

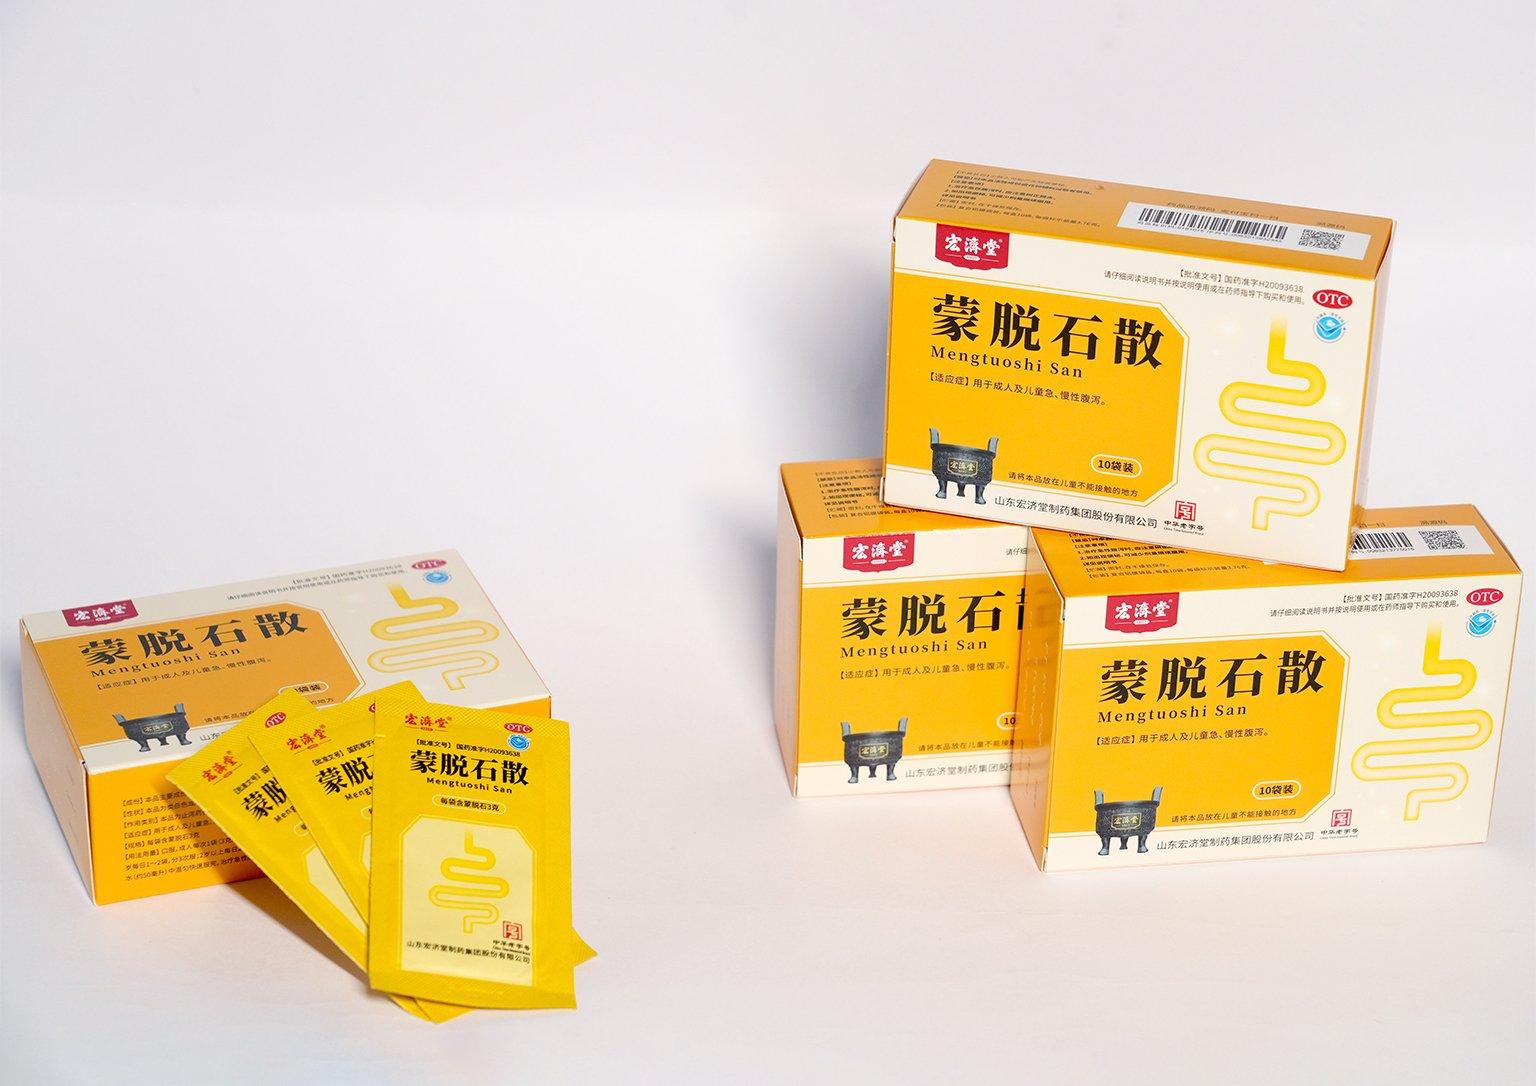

The modern pharmaceutical industry places the highest priority on raw material integrity to ensure the safety and therapeutic outcomes of patients. When procurement departments decide to buy diosmectite powder in bulk, they are essentially setting the foundation for the entire production process of their digestive health portfolio. This natural mineral, known for its powerful ability to coat the intestinal lining and adsorb pathogens, must meet rigid pharmaceutical-grade specifications. By securing a reliable, large-scale supply of high-purity material, manufacturers ensure that their products maintain a consistent clinical performance that satisfies both regulatory standards and consumer expectations for reliability.
Scientific Integrity of Pharmaceutical Minerals
The true value of a mineral in a medical setting is determined by the precision of its processing. Unlike industrial clays, pharmaceutical-grade montmorillonite undergoes extensive purification to remove naturally occurring impurities such as heavy metals, crystalline silica, and other non-active minerals. This refinement process is critical, as the purity of the mineral directly affects its cation exchange capacity and its ability to function correctly within the complex environment of the human digestive tract.
Engineers in the pharmaceutical field analyze these materials using high-level diagnostic tools, including scanning electron microscopy and mineralogical testing, to confirm that every grain meets the required size and purity profile. This scientific approach ensures that the mineral provides a uniform protective barrier, which is essential for managing various gastrointestinal distress symptoms effectively. The commitment to such high analytical standards ensures that the final medication is not only effective but also remains stable throughout its entire shelf life.
Navigating Supply Chain Complexity
The stability of any pharmaceutical product begins with the stability of its supply chain. Reliable mineral procurement is about more than just volume; it is about consistent quality across every batch delivered to the manufacturing facility. When companies work with a specialized montmorillonite pharmaceutical grade supplier, they gain access to a partner who understands the necessity of batch-to-batch consistency and the importance of exhaustive documentation. This partnership model is vital for manufacturers who must comply with the strict regulatory guidelines enforced by global health authorities.
By working with experts who specialize in pharmaceutical minerals, brands can mitigate the risks associated with raw material volatility. These suppliers provide essential certificates of analysis and technical dossiers that prove the mineral is safe, inert, and ready for integration into medicinal formulations. This level of professional transparency allows pharmaceutical manufacturers to focus their resources on innovation and clinical research, knowing that their core ingredients are backed by rigorous quality management systems.
Precision Engineering in Sachet Manufacturing
When it comes to the final product, the convenience and safety of the delivery method are paramount for patient adherence. Utilizing a dedicated diosmectite powder sachet manufacturer allows brands to deliver a product that is perfectly measured and protected against environmental degradation. Sachets are an ideal format for this type of powder, as they safeguard the material from humidity and light, both of which can compromise the structural integrity of the mineral if left exposed.
The manufacturing technology required to fill these sachets involves high-speed, automated equipment that operates under strict sanitary conditions. This ensures that every individual unit contains the exact required dose without the presence of contaminants. The choice of packaging material is also carefully engineered to be chemically inert, meaning it will not interact with the powder, thus ensuring that the product maintains its medicinal properties from the moment it leaves the factory until it is mixed by the patient at the time of use.
Technical Considerations for High-Speed Packaging
Scaling production for international markets requires a deep technical understanding of powder rheology. Fine powders like diosmectite can be challenging to manage in high-speed filling lines, often requiring specialized flow-control technology to maintain dosing accuracy. A professional manufacturer integrates these engineering solutions into their workflow, ensuring that the filling process remains fast and accurate. This level of technical capability is crucial for companies that need to meet large-scale demand without compromising on the quality or weight accuracy of each individual sachet.
Furthermore, these specialized facilities are designed to minimize dust and environmental exposure during the filling process, ensuring the health and safety of the workforce while maintaining the highest level of hygiene. This focus on engineering precision reflects the broader commitment to excellence that defines the most successful companies in the pharmaceutical manufacturing sector.
Future Innovations in Mineral-Based Treatments
As the medical field continues to advance, the potential for mineral-based therapies is growing significantly. We are seeing a move toward more integrated products that combine the natural protective properties of clays with other active ingredients. This evolution requires an even higher level of collaboration between the mineral suppliers and the finished-product manufacturers. The focus on developing new delivery formats and synergistic combinations is pushing the industry to refine its processing techniques even further.
The future of gastrointestinal care is clearly moving toward solutions that are both natural and backed by high-level scientific research. By continuing to invest in purification technology and advanced manufacturing, the industry can ensure that these minerals remain at the heart of modern therapy. The ability to innovate while maintaining safety and efficacy is what will distinguish the leaders in this space in the coming years.
Regulatory Compliance as a Competitive Advantage
Regulatory excellence is not just a burden; it is a significant competitive advantage for pharmaceutical firms. In a market where safety is the number one priority, being able to demonstrate complete traceability—from the raw mineral deposit to the final patient package—builds immense trust. Manufacturers who prioritize this level of transparency with regulators often find that their products gain market approval more efficiently and maintain a stronger reputation among healthcare professionals.
This commitment to compliance extends to all aspects of the supply chain, including ethical mining practices and environmental monitoring. By partnering with suppliers who share these values, pharmaceutical companies create a robust, responsible, and sustainable business model that is well-positioned for long-term growth in the global healthcare landscape.
Conclusion
The successful implementation of mineral-based pharmaceutical products rests on the quality of raw materials and the precision of the manufacturing process. From the careful selection of high-purity minerals to the specialized packaging in sachets, every step is a critical component in delivering consistent therapeutic results to patients. By choosing to work with experts in the field, pharmaceutical companies can ensure that their products are safe, effective, and reliable. As the industry continues to evolve, a focus on transparency, technical excellence, and quality will remain the driving forces behind the development of the next generation of gastrointestinal health solutions.


